
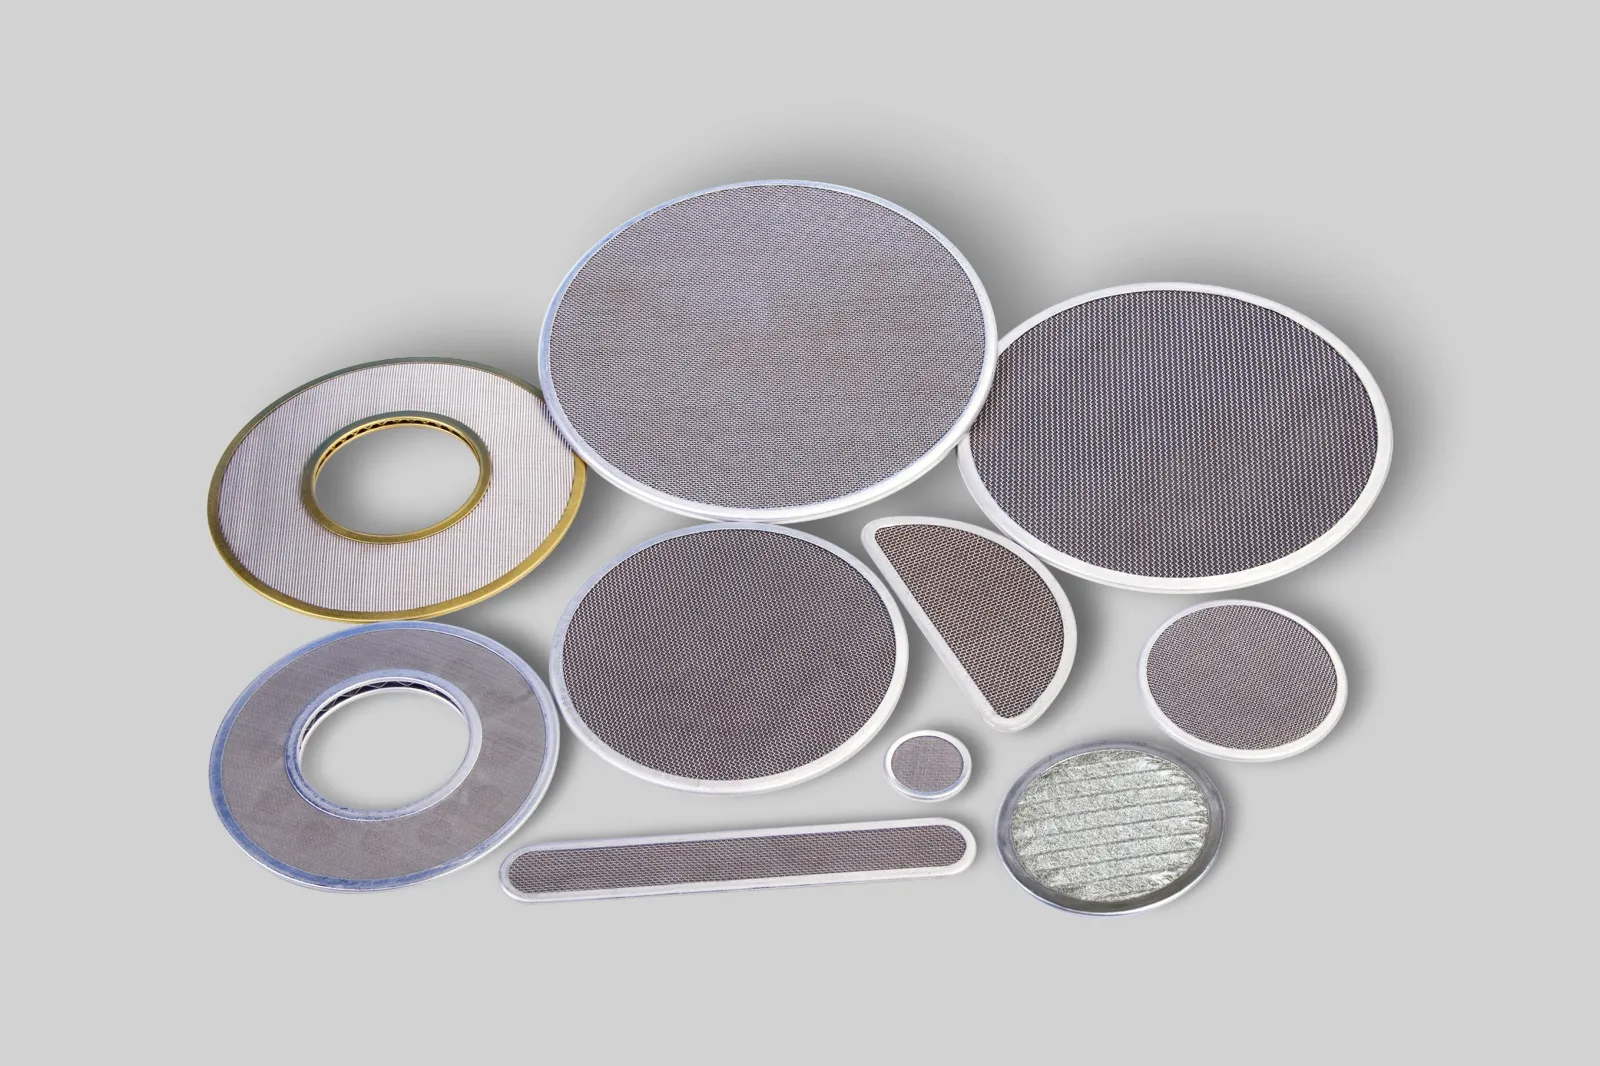
A polymer extrusion line has been running smoothly for hours when the pressure before the filter begins to climb. The operator increases attention to the screen pack, but the next change happens sooner than expected. It is tempting to blame the filter medium immediately. That can waste an entire shift if the real cause sits upstream in the melt, the temperature profile or the way the disc assembly was installed.
Establish what actually changed
Start with a trend, not a single gauge reading. Compare inlet pressure, outlet pressure if available, throughput, melt temperature and the time since the last filter change. Pressure drop is the difference between two measurements taken across the filter. A rising upstream pressure alone can also reflect problems elsewhere in the system.
Record the resin grade, recycled-content proportion, colour masterbatch, additive package and any recent change in supplier or drying practice. A higher contaminant load may shorten filter life, but a viscosity change can raise pressure even without extra particles. Those two mechanisms require different corrective action.
Inspect the discs after a controlled shutdown
Follow the machine maker’s depressurisation and isolation procedure; hot polymer and stored pressure can cause severe injuries. Once safe, document the order and orientation of removed discs. Photograph where deposits have accumulated. A uniform layer of trapped material suggests a different problem from damage concentrated around the seal or a distorted disc edge.
Look for torn mesh, collapsed support layers, uneven clamping and bypass tracks at the perimeter. A filter that looks clean but allows contamination into the product may be suffering from an installation defect rather than insufficient filtration fineness. Do not assume that a finer mesh automatically improves product quality. It also changes resistance and the amount of contaminant the assembly can hold.
Separate contamination from viscosity
If pressure climbs rapidly after changing to a new resin batch, compare the supplier’s melt-flow information and the operating temperature used with the previous material. Polymer degradation can also create gels and deposits; simply raising temperature may worsen the problem. Product samples can help reveal whether black specks, gels or other defects increased along with the pressure change.
A basic investigation works best when only one condition is changed at a time. Changing screen fineness, screw speed and temperature together might restore production, but it makes the cause almost impossible to identify. Keep the trial short enough to avoid creating a large quantity of questionable material.
Selecting a replacement assembly
For a leaf disc filter supplier, a useful enquiry includes the outside and inside diameter, disc thickness, support structure, mesh specification, material of construction, sealing arrangement and the intended polymer process. Drawings are better than photographs for dimension-critical components. Ask about how the assembly is cleaned, whether it can be reused, and what limits the service life of welded joints or support layers.
If the system uses multiple discs, inspect them as a set. Mixed wear or unequal support can cause some units to load differently from others. Confirm that the proposed replacement will fit the existing housing and survive the expected thermal cycling.
Improve the next diagnosis
After a change, record the initial clean-filter pressure drop at the same throughput and temperature used for later comparisons. Track how pressure evolves over time. This creates a baseline for maintenance rather than relying on “it seems to be blocking faster”. Keep one removed filter sample and a corresponding product sample when an unusual event occurs. They can help the technical team decide whether the next investigation belongs in filtration, raw materials or extruder conditions.
Manufacturers such as Howay Filter can discuss component geometry and filtration media with process teams, but the operating history remains essential. Without it, a new disc may simply inherit the same problem as the old one.
The evidence worth keeping
Store the trend plot with the batch record and the removed component identifier. Note the instrument locations and whether gauges were calibrated; a pressure trace is much less useful if nobody knows where the readings came from. If the material contains regrind, record the approximate proportion and how the regrind was handled. Do not describe a filter as 'blocked early' without specifying the starting pressure, threshold and running conditions. A structured record may reveal that short filter life appears only after certain batches or shutdown procedures. That is a much stronger basis for process changes than replacing filtration media repeatedly.
Official website: Howay Filter




Responses (0)